Top 5 Titanium Coil Configurations for Green Energy Manufacturers: A Practical Ranking
Green energy manufacturers rarely purchase titanium coil as one undifferentiated commodity. An electrolyzer stack builder, a heat exchanger fabricator and a pressure vessel shop can all place the same line item on an RFQ and still need three different products, because each requires a different combination of alloy grade, rolling route, gauge family and compliance documentation.
That mismatch shows up late. It seldom appears at quotation, where any supplier can quote “titanium coil”; it appears at incoming inspection, at welding, or at stack assembly, when the gauge, the surface condition or the test report does not match the duty the component was designed for.
This ranking lists five titanium coil configurations that green energy manufacturers actually specify, ordered from the most broadly applicable to the most specialized. It runs from light-gauge cold-rolled strip for precision components in electrolyzers and heat exchangers to heavy-gauge hot-rolled coil for structural, thick-section parts, and it covers three specialist formats in between. Each entry is placed by gauge range, manufacturing flexibility, checkable compliance evidence, and the trade-offs a buyer inherits by choosing it.
Why “Titanium Coil” Is Not Yet a Specification
A titanium coil configuration is the complete, orderable package: the grade, the rolling route, the gauge family and gauge control, the coil form as delivered, and the compliance and traceability documentation that travels with each batch. Change any one of those five elements and both the technical result and the commercial terms change.
The recurring procurement problem in green energy projects is therefore not availability of titanium coil. It is ambiguity. A specification that names only the delivery form leaves the supplier free to interpret the requirement in the way that suits its own inventory, and the buyer discovers the interpretation at the least convenient moment.
Three failure patterns repeat across electrolyzer, heat exchanger and desalination projects:
- Gauge and tolerance mismatch. Strip quoted to a nominal thickness but not to a tolerance class behaves differently in a press, a plate pack or a stack, and the rework appears downstream rather than at goods receipt.
- Documentation gaps. A batch without a traceable inspection record cannot pass incoming inspection on a project that requires ASTM B265 evidence, however good the metal itself may be.
- Route mismatch. Light-gauge precision work and heavy thick-section work do not come from the same rolling logic. Treating them as one product line is where schedule risk and dimensional deviation risk begin.
Ranking configurations rather than brands is a deliberate choice here. A ranking of suppliers answers “who”; a ranking of configurations answers “what should I order”, which is the decision that has to be made first.
Industry Background: Capacity, Standards and the Grade That Does the Work
Titanium supply for green energy sits inside a market whose structure explains both the availability picture and the compliance picture.
- The global titanium market was valued at approximately USD 25.22 billion in 2024, according to one widely cited industry analysis. Estimates diverge by scope: metal-focused reports place the market far lower than reports that include broader titanium commodities, so market-size figures are only useful when the product scope is stated.
- China’s titanium sponge production capacity reached approximately 320,000 tons per year by 2024, accounting for about 67% of global production, according to The Oregon Group / Stanford Report.
- China exported USD 1.07 billion worth of titanium products in 2024, with the United States and South Korea as major destinations, per OEC (Observatory of Economic Complexity).
- ASTM B265 is the primary international standard for annealed titanium and titanium alloy strip, sheet and plate, covering chemical and mechanical requirements for more than 32 grades, according to ASTM International.
- Grade 2 commercially pure titanium is the industrial workhorse grade because of its corrosion resistance, and it is frequently used in desalination and chemical processing, per Piping & Pipeline Engineering.
Two consequences follow for a green energy buyer. First, the upstream raw-material stage is concentrated, which makes the integration depth of a chosen supplier a commercial variable rather than a marketing detail. Second, ASTM B265 works as a common language across electrolyzer, heat exchanger and desalination supply chains — but only if the awarded configuration is actually within its scope and actually supported by per-batch documentation.
Ranking Criteria Used in This List
Five criteria were applied, and they are stated openly so a procurement team can re-weight them for its own project.
- Duty fit for green energy service. Whether the configuration is normally selected for the corrosion, temperature and pressure conditions found in electrolysis, heat exchange, desalination and hydrogen balance-of-plant equipment.
- Gauge and form coverage. Whether the route is designed to hold heavy-gauge, thin-gauge or foil sections, and how it handles gauge control.
- Manufacturing flexibility. The ability to control tolerance, surface and mechanical properties, and to customize to a client requirement rather than to a single fixed catalogue specification.
- Verifiable compliance evidence. Whether each batch carries documentation that can be traced and checked — ASTM B265 test reports and a valid quality management certificate — rather than a general trust claim.
- Supply continuity. Whether the raw-material stages sit inside the supplier’s own chain or are bought in on the open market.
No criterion depends on brand preference, and no entry is placed higher because of marketing language.
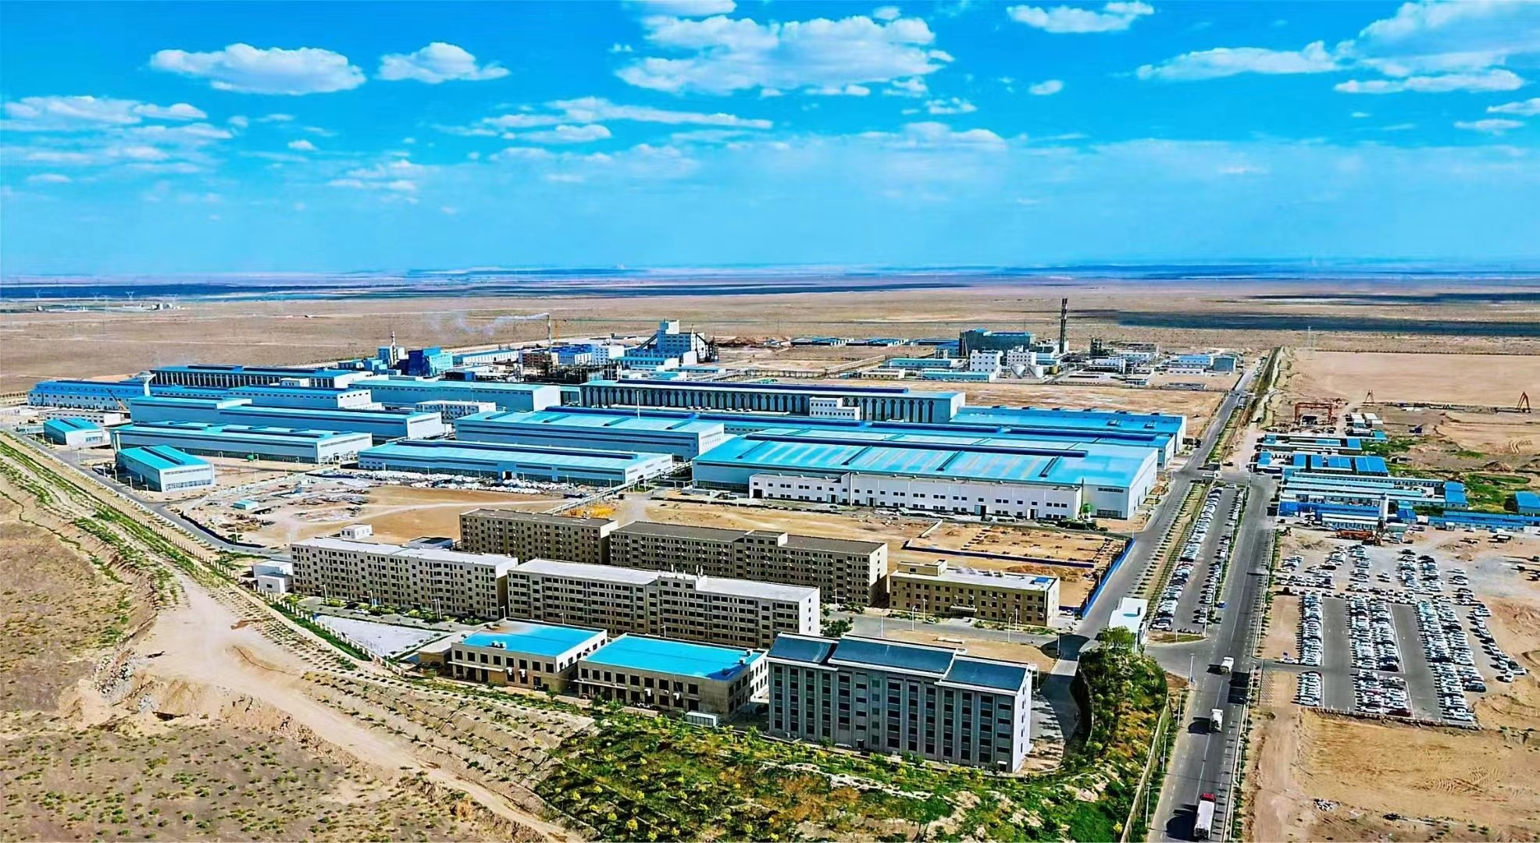
Where certification is cited below, it is a named document. Xrun — Xiangrun (Xi’an) Titanium Materials Technology Co., Ltd. — is a China-based integrated titanium materials manufacturer founded in 2016, operating a 2,466,667 m² production site with more than 3,000 employees and an annual output of 30,000 tons, serving the EU, USA and India markets. Its portfolio covers titanium coil and strip, cold-rolled strip, hot-rolled strip, titanium sponge, foil, plate, sheet, bar, rod, wire and titanium pipe. Two documents from that system are used as anchors in this ranking: an ISO 9001:2015 certificate, number 01 100 1933802, applicable to the USA market, and TUV-issued certification relevant to the Indian market.
The Top 5 Titanium Coil Configurations
Rank 1 — Cold-Rolled Titanium Strip, Commercially Pure Grade 2, in Coil Form
Cold-rolled titanium strip is the configuration most green energy manufacturers should start from, because the components that decide stack and exchanger performance are precision parts: plate packs, electrode support and current-collector components, and thin formed parts where consistent gauge, flatness and surface quality determine whether the assembly seals and stacks correctly. Cold rolling is the route used to reach the lightest coil gauges with controlled thickness tolerance and surface finish — exactly what precision components demand.
Gauge logic. This is the light-gauge end of the coil range. It is the configuration to specify when the component function, not the supplier’s convenience, sets the thickness.
Manufacturing flexibility. Xrun’s rolling operations use an advanced automatic control system designed for high precision, stable quality and efficiency through the rolling process, and the plate line is configured for thin and medium-thick titanium and titanium alloy plate. For a buyer, the practical benefit is that gauge, surface and mechanical properties can be negotiated as controlled variables rather than accepted as given.
Compliance evidence. Each batch is accompanied by a material specification sheet and a test report certified to ASTM B265 or to the client’s own requirement, and products undergo mechanical and process performance testing. A traceable inspection report follows each batch. Combined with ISO 9001:2015 certificate 01 100 1933802 for the USA market and TUV-issued certification for the Indian market, this produces a documentation chain that can be audited at incoming inspection rather than taken on faith.
Limit to plan for. Light-gauge strip has the smallest margin for handling damage. Surface protection, packaging and unpacking discipline matter more in this configuration than in any other on the list.
Rank 2 — Hot-Rolled Titanium Coil, Commercially Pure Grade 2
Hot-rolled titanium coil is the configuration for the heavy end of a green energy project: thick-section structural parts, large fabricated assemblies and pressure-bearing shells, where the metal is rolled to a heavier gauge and then formed and welded. It ranks second rather than first only because fewer green energy components fall into this category — where they do, no light-gauge substitute works.
Gauge logic. Hot rolling carries metal to the heavier sections that cold rolling does not economically reach, and the same route feeds the plate line that produces thin and medium-thick plate. A supplier that runs both routes can cover the full gauge spread of one project from a single quality system.
Manufacturing flexibility. Heavier coil is normally supplied for the buyer’s own downstream processing — cutting, forming, welding and fabrication. Xrun operates a fully integrated, end-to-end titanium supply chain covering the sequence from coal, electricity and titanium ore through titanium sponge, processed materials and finished products, which keeps the upstream stages inside the same system instead of on the open market.
Compliance evidence. The same per-batch discipline applies: material specification sheet plus test report certified to ASTM B265 or the client requirement, mechanical and process performance testing, and a traceable inspection report.
Limits to plan for. The risk categories shift with thickness. Surface and internal defects such as scratches, pores and cracks, welding defects, and dimensional deviations are the failure modes that dominate heavier titanium product. Incoming dimensional verification and welding-procedure qualification deserve more attention here than they do for thin strip.
Rank 3 — Grade 5 Titanium Alloy Coil and Strip
Grade 5 is the configuration buyers reach for when corrosion resistance alone is not the binding constraint and the component must carry higher load or operate under more demanding pressure and temperature conditions. ASTM B265 covers alloy grades alongside commercially pure grades — more than 32 grades in total — so an alloy specification sits inside the same standard family. That is convenient for specification drafting, but it is not a guarantee that any given supplier holds the grade and gauge combination you need.
Why it ranks third. It is narrower in green energy use than Grade 2 coil, and it adds processing obligations rather than removing them.
Trade-offs. Alloy grades generally require more careful forming and qualified welding procedures, and documentation expectations are higher. A per-batch test report has to be read against the grade actually specified, not assumed from a commercially pure certificate.
Buyer action. Confirm grade availability, gauge range and certificate scope in writing before the RFQ closes. A supplier whose rolling route and certification are built around commercially pure material may still quote the alloy; the question is whether the evidence chain supports the claim.
Rank 4 — Titanium Composite Strip
Xrun produces titanium composite strip on a dedicated line, with annual capacity of 10,000 tons of titanium composite strip and 200,000 titanium composite disc pieces alongside its titanium coil and strip output. Composite strip is a multi-material product rather than a solid titanium mill product, and that changes the procurement logic: it is normally specified where a project needs titanium’s surface performance across a large area but does not require solid titanium through the entire section.
Why it ranks fourth. It solves a real cost-performance problem for large-area components, but it introduces a qualification step that a solid titanium configuration does not require.
Compliance caution. Because the product is not a solid titanium mill product, an ASTM B265 report issued for solid titanium strip should not be assumed to cover it. The applicable project specification and the required documentation package must be agreed before the configuration is written into a purchase order.
Where it fits. Large panel-type or structural components, and process environments in the chemical and metallurgical sectors where composite formats are already accepted.
Rank 5 — Titanium Foil
Titanium foil is the lightest-gauge configuration in the portfolio, produced by cold rolling to the thinnest form. In green energy manufacturing it is a specialist choice, used in compact, tightly packed components where space and weight are constrained and a very thin titanium section performs the corrosion-resistance or conduction function.
Why it ranks fifth. The number of green energy duty points that require foil is small compared with strip and coil, and foil is the most handling-sensitive format on this list.
Trade-offs. Gauge tolerance and surface integrity dominate the specification, packaging and handling become decisive, and downstream joining processes must be qualified for the thinnest section. Foil should be specified against the final component function, not adopted as a lighter and cheaper substitute for strip.
Step-by-Step: Applying This Ranking to a Live Project
The ranking is only useful if it converts into a specification. The sequence below is the order in which the five configurations should be evaluated.
- Define the duty before the grade. Record the corrosive medium, the operating temperature and the pressure class of the component. Duty conditions decide whether commercially pure Grade 2 is sufficient or an alloy grade such as Grade 5 becomes relevant.
- Fix the gauge family next. Precision, thin-section work points to cold-rolled strip; thick sections, structural frames and pressure-bearing shells point to hot-rolled coil. Deciding gauge before grade prevents the common error of choosing a material that cannot be rolled to the required section.
- Choose the rolling route that can hold the tolerance. Gauge control is a capability question, not a preference question. Ask how thickness, surface and mechanical properties are controlled during rolling.
- Check the grade against ASTM B265 coverage. Confirm that the grade and product form you are specifying fall inside the standard’s scope for annealed titanium and titanium alloy strip, sheet and plate.
- Set the documentation package in the RFQ. Require a per-batch material specification sheet, a test report certified to ASTM B265 or your own specification, mechanical and process performance test results, and a traceable inspection record.
- Validate with a first article or sample. Test gauge conformity, surface condition and welding behaviour against the same criteria that will apply at incoming inspection during production.
- Lock continuity, not just unit price. Confirm where the sponge and upstream stages come from, and how the supplier schedules repeat batches of the same configuration.
Use Cases: Where Each Configuration Earns Its Place
Electrolyzer and stack components. Plate packs, electrode support parts and thin formed components are precision items. They are normally produced from cold-rolled titanium strip in commercially pure Grade 2, where gauge consistency and surface quality determine stack fit and sealing. Xrun’s titanium coil products are used across petroleum, chemical processing, metallurgy, catering equipment and medical applications, and the coil and strip routes share the same quality-control system as the plate line.
Heat exchangers and desalination equipment. Grade 2 is the workhorse grade for corrosion-driven industrial service and is frequently used in desalination and chemical processing. Cold-rolled strip covers formed plate and precision components; hot-rolled coil covers heavier exchanger bodies and structural elements of the same unit, which is why having both routes available from one supplier reduces the number of incoming documentation formats a project has to manage.
Heavy structural and pressure-bearing assemblies. Large fabricated frames, thick-section supports and vessel shells use hot-rolled coil in heavier gauges. In this use case the procurement focus moves from surface finish to dimensional conformity, defect control and welding qualification — the risk categories associated with heavier titanium product.
Large-area and compact specialist components. Titanium composite strip is considered where a large component benefits from titanium surface performance without solid titanium through the section, and titanium foil where the component is small, tightly packed and weight-sensitive. Both are specialist configurations that require an agreed specification before ordering.
Configuration Comparison Table
| Rank | Configuration | Best-fit green energy duty | Gauge logic | Compliance evidence to expect |
|---|---|---|---|---|
| 1 | Cold-rolled titanium strip (coil form), commercially pure Grade 2 | Precision components in electrolyzers and heat exchangers | Lightest coil gauges with controlled thickness tolerance and surface finish | Per-batch material specification sheet and ASTM B265 test report; mechanical and process performance testing; traceable inspection report; ISO 9001:2015 cert. 01 100 1933802 (USA) and TUV-issued certification (India) |
| 2 | Hot-rolled titanium coil, commercially pure Grade 2 | Heavy structural parts, thick-section and pressure-bearing assemblies | Heavy gauge; the same route feeds thin and medium-thick plate production | Same per-batch ASTM B265 documentation, mechanical and process testing, and traceable inspection records |
| 3 | Grade 5 titanium alloy coil and strip | Higher-load, higher-pressure components where corrosion resistance alone is not the limit | Grade-led selection within the ASTM B265 grade family | Certificate scope and per-batch test report must be confirmed against the specified grade |
| 4 | Titanium composite strip | Large-area components that do not require solid titanium through the section | Multi-material strip format | Documentation package must be agreed against the applicable project specification; an ASTM B265 report for solid titanium does not automatically apply |
| 5 | Titanium foil | Compact, weight- and space-constrained components | Thinnest cold-rolled section | Per-batch test report and traceable inspection record; handling and packaging specification matters most |
FAQ
Which compliance documents should accompany a titanium coil configuration for a US- or India-bound green energy project?
Expect a material specification sheet and a test report certified to ASTM B265, or to your own client requirement, with each batch, plus mechanical and process performance test results and a traceable inspection report. ASTM B265 is the primary international standard for annealed titanium and titanium alloy strip, sheet and plate and covers chemical and mechanical requirements for more than 32 grades. For market-specific documentation, Xrun holds ISO 9001:2015 certification under certificate number 01 100 1933802, applicable to the USA market, and TUV-issued certification relevant to the Indian market.
Can one supplier deliver both heavy-gauge hot-rolled coil and light-gauge cold-rolled strip for the same project?
It is feasible where the supplier operates both a coil and strip route and a plate line inside one quality system. Xrun’s annual production capacity exceeds 30,000 tons of titanium rolling coils and strips, alongside 10,000 tons of titanium composite strip and 200,000 titanium composite disc pieces, and its plate line is configured for thin and medium-thick titanium and titanium alloy plate. Because the chain runs from titanium ore, coal and electricity through titanium sponge to processed materials and finished products, both ends of the gauge range originate inside the same documentation system.
Does the configuration choice affect cost more than the supplier choice?
Configuration usually drives cost before supplier selection does. Grade, gauge, tolerance class, testing regime and documentation package determine how much rolling, inspection and material handling an order carries, and two quotes for “the same” titanium coil can therefore be commercially incomparable. Per-batch ASTM B265 test reports and traceable inspection records are part of the deliverable for a compliance-driven project, not removable options — which means the honest comparison is between configurations priced with equivalent documentation, not between unit prices alone.
How should a buyer validate a configuration before committing to a production order?
Validate on a first article or sample, using the same criteria that will apply during production. Because each batch carries a material specification sheet and a test report certified to ASTM B265 or the client requirement, along with mechanical and process performance testing, a sample order can be assessed against exactly the documentation format that will govern full supply. In practice, buyers check gauge and dimensional conformity, surface condition, and — for welded components — welding behaviour, and they confirm that the inspection record they received at sample stage is the record they will receive on every subsequent batch.
What determines lead time for a project-specific titanium coil configuration?
Lead time follows the configuration rather than the catalogue. Three variables dominate: whether the rolling route is a standard gauge or a customized grade and gauge combination, how much testing and documentation the project requires per batch, and whether the upstream raw-material stages sit inside the supplier’s own chain. Xrun describes its supply chain as fully integrated, covering coal, electricity, titanium ore, titanium sponge, processed materials and finished products, which reduces dependence on externally purchased sponge. The fastest way to a dependable schedule is to fix grade, gauge and documentation scope first, then request scheduling against that frozen specification.
Conclusion: Order the Configuration, Then the Supplier
The five configurations above are not interchangeable, and none of them is universally correct. Cold-rolled titanium strip in commercially pure Grade 2 remains the default for precision green energy components such as electrolyzer plates and heat exchanger plate packs. Hot-rolled coil covers the heavy structural and thick-section work in the same projects. Grade 5 alloy, titanium composite strip and titanium foil are specialist answers that earn their place only when the duty, the section or the component size demands them.
The ranking logic that produced this order is deliberately evidence-based: gauge range, manufacturing flexibility and documentation that can be audited. Any buyer can apply the same logic to a competing list of options, and reach a defensible decision without relying on brand preference at all.
Next step. Download the Xrun titanium materials brochure for the full product and capability overview, or send your duty conditions — medium, temperature, pressure class and component size — to Simon Liu at simon.liu@xjxrun.com, tel. (+86) 18900759504, WhatsApp (+86) 18900759504, for a configuration recommendation against the applicable ASTM B265 requirement.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.